Key Takeaways
- First define the symptom before replacing parts. A compressor that never loads is a different fault from one that loads normally but delivers weak airflow. If the engine runs but the compressor never develops normal internal pressure, start with the Compressor Will Not Load Troubleshooting Guide rather than treating it as a low-capacity problem.
- Compare pressure at more than one location. Low separator/sump pressure and low outlet pressure point toward intake, loading or compressor-capacity problems; high internal pressure with low outlet pressure points toward the discharge path. The Minimum Pressure Valve Troubleshooting Guide explains this important difference.
- A clogged intake filter, partially opening inlet valve, air leak or excessive air demand should normally be checked before airend wear. The broader Portable Screw Air Compressor Troubleshooting Guide covers the main field failure patterns.
- Normal compressor pressure does not guarantee normal pressure at the tool. Long hoses, small internal diameters, restrictive couplings and inline equipment can create substantial pressure drop. The Compressed Air System Design Guide explains how hose and piping losses affect field performance.
- Do not judge compressor capacity from a pressure gauge alone. A proper performance check compares measured airflow with rated FAD at the same working pressure. The CFM vs FAD vs SCFM vs ACFM Guide explains why rating basis matters when comparing actual compressor output.
A portable screw compressor can start normally, reach operating speed and show no major alarm while still leaving the operator with one simple complaint:
“The air is weak.”
On a drilling rig, the DTH hammer may slow down.
During sandblasting, the nozzle may lose cleaning force.
Pneumatic tools may work normally until several users start at the same time.
Or the compressor may simply take much longer than before to reach operating pressure.
These symptoms are often described as the same problem, but they can come from very different parts of the system.
The compressor may genuinely be producing too little air.
Or it may be producing the correct air, only to lose pressure through a leaking or undersized delivery system.
The most efficient diagnostic sequence is therefore:
Confirm the Pressure Pattern → Check Engine Speed → Check Intake Restriction → Verify Inlet Valve Opening → Check Leaks and Demand → Measure Hose Loss → Correct for Site Conditions → Test Actual FAD → Evaluate Airend Condition
Airend overhaul should be near the end of that sequence, not the beginning.
First Confirm What “Low Pressure” Actually Means
Before opening any component, measure where the pressure is being lost.
Operators often report only:
“Pressure is low.”
That is not yet a diagnosis.
A useful first comparison is:
| Pressure Pattern | Most Likely Diagnostic Direction |
|---|---|
| Sump low + outlet low | Intake restriction, partial loading, low engine speed, insufficient compressor output |
| Sump builds slowly + outlet low | Restricted intake, partially opening inlet valve, control leak |
| Sump high + outlet very low | MPV or downstream discharge restriction |
| Compressor outlet normal + tool pressure low | Hose, fittings, filter, regulator, leaks or excessive tool demand |
| Pressure normal unloaded but falls sharply under use | Demand exceeds available FAD or distribution system is restrictive |
This simple comparison prevents many unnecessary repairs.
A compressor producing high internal vessel pressure is clearly compressing air. If almost no pressure reaches the outlet, the primary problem is unlikely to be a worn airend.
Conversely, if both internal and outlet pressure stay below normal while the compressor is supposedly fully loaded, the investigation needs to move upstream toward intake, control and compressor capacity.
Check Engine Speed Before Blaming the Compressor
A portable diesel screw compressor depends on the prime mover reaching the correct loaded operating speed.
If the engine cannot reach commanded RPM because of:
- fuel restriction;
- engine derating;
- control problems;
- high altitude;
- excessive temperature;
- engine-protection limiting;
the airend cannot turn fast enough to produce rated FAD.
This can create a misleading symptom.
The compressor appears loaded.
The inlet valve may be open.
There may be no obvious leak.
But the machine still produces less air than expected.
Check actual loaded engine RPM against the machine specification before moving deeper into the compressor.
A rotary screw compressor’s airflow is strongly linked to airend speed. If the airend is being driven below its intended loaded speed, replacing filters or valves will not restore rated capacity.
A Clogged Intake Filter Can Starve the Airend
The air filter is one of the simplest components in the compressor and one of the first that should be checked.
A screw compressor cannot deliver air that it cannot inhale.
Dusty quarry, mining and drilling environments can load an intake element much faster than clean industrial installations.
As restriction rises, the airend sees lower pressure at its inlet.
The machine must then work with less available intake air, which can reduce output and increase operating effort.
Typical signs include:
- slow pressure build-up;
- reduced FAD under full load;
- intake restriction indicator showing excessive restriction;
- increased fuel consumption for the same work;
- improvement after installing a clean filter.
Do not judge the filter only from how dirty the outside looks.
Use the compressor’s restriction indicator or the specified differential-pressure method where available.
Also inspect:
air cleaner → intake hose → inlet valve
A collapsed hose, internal delamination or loose intake connection can create similar symptoms.
The Inlet Valve May Open—But Not Fully
The inlet valve controls how much atmospheric air enters the screw element.
When the compressor loads, the valve should move into the position required for full air intake.
A completely stuck-closed valve usually produces a clear no-load condition.
A partially opening inlet valve is more difficult to diagnose.
The machine may:
- accelerate to loaded speed;
- build some pressure;
- look normal on the controller;
- still deliver only part of its rated capacity.
Possible causes include contamination, worn actuator seals, sticking internal parts, damaged linkage or incorrect control-air conditions.
This is why simply confirming:
“The inlet valve moves.”
is not enough.
The real question is:
Does the valve reach the correct fully loaded position?
Before condemning the valve mechanically, verify the pneumatic or electrical control signal reaching its actuator.
A correct load command with the wrong actuator condition may still be a solenoid or control-air problem rather than a failed inlet valve.
Air Leaks Can Make a Healthy Compressor Look Too Small
Sometimes nothing is wrong with the compressor.
The machine produces its rated airflow, but a significant portion never reaches the tool.
Common leak points include:
- hose couplings;
- quick-connect fittings;
- cracked flexible hoses;
- manifold connections;
- drain valves;
- pressure regulators;
- worn seals;
- auxiliary air branches left open.
Small leaks become especially expensive in a high-flow portable system because the compressor continuously replaces the escaping air.
The simplest diagnostic method is to reduce or isolate downstream demand where the operating procedure allows.
If the compressor reaches normal pressure easily with the downstream system isolated but struggles after hoses and tools are connected, the problem has moved outside the compressor package.
For difficult leaks, ultrasonic detection or a properly installed flow meter can help distinguish:
compressor capacity problem
from:
air being lost after compression.
Confirm That Demand Has Not Increased
Before diagnosing a mechanical failure, ask one operational question:
Has anything changed on the jobsite?
A compressor that was large enough last month may suddenly look weak because the air demand increased.
Examples include:
one DTH rig → two air users
smaller blast nozzle → larger nozzle
30 m hose → 80 m hose
one pneumatic tool → several tools
or:
larger DTH hammer
If total demand exceeds compressor FAD, the system pressure drops under load even when the compressor is operating correctly.
This creates a characteristic pattern:
Pressure recovers when tools stop → drops again when full demand returns
That behavior should trigger a demand and distribution check before the compressor is dismantled.
Hose Pressure Drop Can Hide Good Compressor Performance
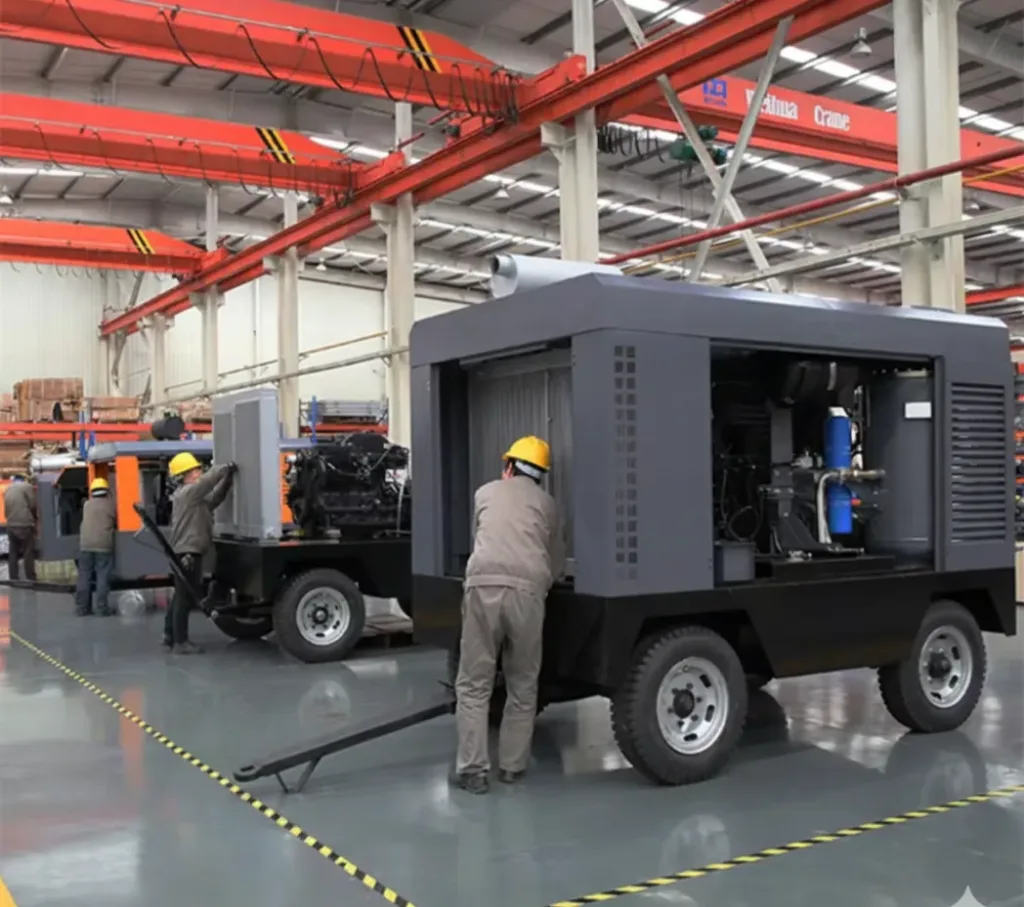
Portable compressors often work far from the actual tool.
The compressor may sit safely on a road or bench while a drill, shotcrete nozzle or pneumatic tool operates tens of meters away.
Pressure is lost as air moves through:
hose walls + fittings + couplings + valves + regulators
The amount of loss depends heavily on airflow velocity.
A hose that works well at 200 CFM can become severely restrictive at 500 CFM.
A published portable-compressor hose-loss table provides a useful example.
A 1-inch, 50-foot hose carrying approximately 300 CFM at 100 PSI can lose close to 10 PSI across the hose.
That is nearly:
0.7 bar
lost before fittings, couplings or the tool are considered.
The compressor gauge can therefore show healthy pressure while the operator reports weak performance.
The correct test is simple:
Measure pressure at the compressor
Record discharge pressure while the system is under normal full demand.
Measure pressure near the tool
Install a suitable gauge as close as practical to the tool inlet and repeat the same operating condition.
Compare the two readings
The difference is the distribution pressure loss.
If compressor discharge pressure is normal but tool pressure is poor, increasing compressor pressure should not be the first response.
First check:
- hose ID;
- hose length;
- couplings;
- restrictive fittings;
- regulators;
- filters;
- water separators;
- unnecessary elbows or branches.
A larger hose can sometimes solve a “low compressor pressure” complaint without touching the compressor at all.
Separator and Discharge Restrictions Can Also Reduce Output
The intake side is not the only place restriction occurs.
A clogged separator element or restrictive discharge component can also create abnormal pressure patterns.
The key is to compare pressure locations.
If internal separator-vessel pressure is considerably higher than downstream pressure, the compressor is already generating pressure internally.
The problem is in the path out of the vessel.
Possible areas include:
separator element
minimum pressure valve
discharge check valve
downstream valve
or:
restricted inline equipment
Do not confuse this with a weak airend.
A worn airend tends to reduce the machine’s ability to generate normal airflow or pressure in the first place.
A downstream restriction creates pressure before the restriction and low pressure after it.
That difference is extremely useful diagnostically.
Altitude and Temperature Can Reduce Available Margin
Portable compressors rarely operate under laboratory conditions.
A machine selected at sea level may later work at a mine several thousand meters above sea level.
At altitude, atmospheric pressure and air density decrease.
For a diesel portable compressor, the engine also receives less oxygen.
Depending on engine design and altitude-compensation capability, available engine power may be reduced.
High ambient temperature creates another challenge because:
- inlet air becomes less dense;
- engine cooling load increases;
- compressor-oil cooling becomes more difficult;
- protective controls may limit operation if temperatures rise too far.
This does not mean every high-altitude compressor automatically loses the same percentage of FAD.
Different engines, airends and control systems respond differently.
Use the manufacturer’s altitude and temperature performance limits instead of applying one universal correction factor.
From a troubleshooting perspective, altitude becomes especially relevant when:
the machine performed normally at a lower site but becomes weak after being moved to elevation.
Before replacing compressor components, confirm whether the machine is still operating inside its specified environmental envelope.
Airend Wear Should Be a Diagnosis of Exclusion
Airend wear is real, but it is one of the most expensive diagnoses on the list.
It should therefore come after easier external causes have been eliminated.
The screw airend relies on very small internal clearances.
As bearings, rotor surfaces or internal components wear, internal leakage can increase.
Some compressed air moves back toward the low-pressure side rather than leaving as useful output.
The result can be:
- gradually decreasing FAD;
- longer pressure build time;
- inability to support tools that the machine previously handled;
- normal-looking control operation;
- no obvious external leak.
The word gradually matters.
A compressor that suddenly loses half its output from one shift to the next is less likely to have experienced ordinary progressive airend wear than one whose performance has declined over thousands of operating hours.
Do not diagnose the airend from operating hours alone.
A more defensible method is:
clean intake → verified inlet opening → correct engine RPM → leaks eliminated → distribution isolated → measure actual output
Only after these checks should measured capacity be compared with rated FAD.
A Practical Performance Test
A useful low-output test should reproduce a known operating condition as closely as possible.
Before testing, confirm that:
- the compressor is at operating temperature;
- filters are serviceable;
- oil level is correct;
- the inlet valve reaches full-load position;
- engine RPM is correct;
- major external leaks are eliminated;
- the machine is operating at the specified test pressure.
Then measure:
| Measurement | What It Tells You |
|---|---|
| Separator/sump pressure | Whether pressure is being produced internally |
| Outlet pressure | Whether air is leaving the compressor normally |
| Tool-end pressure | Distribution-system loss |
| Engine RPM | Whether the airend is being driven correctly |
| Intake restriction | Whether the compressor is starved for inlet air |
| Flow/FAD | Whether actual capacity matches expected output |
| Ambient temperature | Whether heat affects performance |
| Site altitude | Whether derating must be considered |
A pressure gauge alone cannot confirm airflow.
A compressor can hold pressure with little demand yet fail badly once a large air user opens.
The performance test therefore needs to be done under realistic load.
Diagnostic Case 1: Same Complaint, Two Completely Different Faults
Consider two operators who both report:
“The compressor runs, but we have almost no air.”
Machine A shows:
separator pressure low
outlet pressure low
This points toward:
intake / loading / low-speed / compressor-output diagnosis
Machine B shows:
separator pressure high
outlet pressure near zero
This points toward:
MPV or discharge restriction
The operator’s complaint is identical.
The pressure pattern is completely different.
This is why measuring pressure location is more useful than immediately replacing the component most commonly blamed for the symptom.
Diagnostic Case 2: Compressor Gauge Normal, Tool Still Weak
Consider a portable compressor operating at approximately:
100 PSI
through:
50 ft of 1-inch hose
with airflow around:
300 CFM
Published portable-compressor hose-loss data shows that a hose in this range can lose nearly:
10 PSI
before additional couplings and fittings are included.
That means the compressor itself may be perfectly healthy while the tool receives only about:
90 PSI or less
under full demand.
Increasing compressor discharge pressure may temporarily mask the problem.
A larger hose or lower-restriction distribution path addresses the actual cause.
This is an important field lesson:
Low pressure at the tool does not automatically mean low pressure at the compressor.
Repair Only After the Fault Is Isolated
Once the failure has been identified, repair the component responsible rather than replacing parts in sequence.
Typical corrective actions include:
| Confirmed Cause | Typical Corrective Direction |
|---|---|
| Intake filter restriction | Clean or replace according to manufacturer procedure |
| Damaged intake hose | Repair or replace |
| Inlet valve not fully opening | Inspect actuator, control circuit and mechanical valve |
| External air leak | Repair hose, seal, coupling or valve |
| Excessive demand | Reduce simultaneous demand or increase compressor capacity |
| Undersized hose | Increase hose ID or reduce hose length |
| Clogged separator | Replace according to pressure differential and service procedure |
| MPV/discharge restriction | Inspect and service discharge path |
| Altitude derating | Use approved high-altitude configuration or correctly sized compressor |
| Measured FAD below rating after all other checks | Inspect airend and drive system |
Do not open filters, valves, separator vessels or oil circuits while the compressor is pressurized.
Before internal service:
shut down → isolate → depressurize → verify zero stored pressure → follow the machine service procedure
Compressed air and hot compressor oil can cause serious injury if components are opened under pressure.
Common Mistakes During Low-Pressure Troubleshooting
- Replacing the airend first. External restrictions, leaks and inlet problems are much more practical first checks.
- Looking only at the dashboard pressure. Measure sump, outlet and tool-end pressure.
- Testing with no air demand. A compressor can look normal unloaded and collapse under full flow.
- Increasing set pressure to hide hose loss. This wastes energy and does not correct the restriction.
- Ignoring intake restriction. A loaded filter can reduce capacity without creating a dramatic alarm.
- Assuming the inlet valve is either open or closed. Partial opening is a common low-capacity condition.
- Ignoring changed jobsite demand. A larger tool may simply require more FAD.
- Ignoring altitude. A compressor moved to a high-elevation project may have less operating margin.
- Diagnosing airend wear from hours alone. Confirm actual FAD after eliminating external causes.
Practical Troubleshooting Checklist
When a portable screw compressor delivers weak air, record:
- Rated FAD: m³/min or CFM.
- Rated working pressure: bar or PSI.
- Current separator/sump pressure.
- Current outlet pressure.
- Pressure at the tool under load.
- Loaded engine RPM.
- Intake-filter restriction reading.
- Inlet-valve position under full load.
- Visible or detected air leaks.
- Hose ID and total length.
- Number and size of fittings/couplings.
- Connected tool demand.
- Site altitude.
- Ambient temperature.
- Compressor operating hours.
- Recent maintenance or configuration changes.
Those readings allow the problem to be narrowed down systematically instead of replacing components by guesswork.
Final Recommendation
Low airflow and low pressure in a portable screw compressor should be treated as a system symptom, not automatically as a compressor failure.
Start by determining where the pressure is being lost.
Then work through the system in a logical order:
Pressure Pattern → Engine Speed → Intake Filter → Inlet Valve → Air Leaks → Actual Demand → Hose Pressure Drop → Site Conditions → FAD Test → Airend
The key diagnostic distinctions are simple:
Low compressor pressure → investigate compressor capacity and control.
Normal compressor pressure + low tool pressure → investigate distribution.
High internal pressure + low outlet pressure → investigate the discharge path.
Normal controls + gradually declining measured FAD → consider airend condition.
The most expensive component should not be the first component replaced.
The most reliable repair is the one supported by measurements.
FAQ
Why is my screw compressor running but producing low pressure?
Common causes include intake restriction, a partially opening inlet valve, air leaks, excessive air demand, low engine RPM, downstream restriction or actual compressor-capacity loss.
Can a dirty air filter cause low compressor pressure?
Yes. A severely restricted intake filter reduces the amount of atmospheric air reaching the airend and can cause slow pressure build-up and reduced airflow.
Can the compressor show normal pressure while the tool receives low pressure?
Yes. Long or undersized hoses, restrictive fittings, filters, regulators and air leaks can create significant pressure drop between the compressor and the tool.
How do I know if the inlet valve is causing low airflow?
Confirm that the compressor is receiving a load command and that the correct control condition reaches the actuator. If the valve still fails to move to the specified full-load position, the valve or actuator becomes a stronger suspect.
How do I know if the airend is worn?
Airend wear should be considered after verifying clean intake, correct inlet-valve opening, normal engine RPM, no major leaks and acceptable downstream restriction. Measure actual compressor output at a known pressure and compare it with the rated FAD.
Does high altitude reduce portable compressor performance?
It can. Air density and atmospheric pressure decrease with altitude, and diesel-engine power may also be affected. The actual derating depends on the specific engine and compressor design.
Should I increase compressor pressure if the tool feels weak?
Not immediately. First measure pressure at both the compressor and the tool. If the loss is in the hose or distribution system, increasing compressor pressure only hides the real problem and increases operating cost.
What is the first test for low compressor airflow?
Start with separator/sump pressure, outlet pressure and tool-end pressure under load. Those three measurements quickly show whether the problem is inside the compressor or downstream.
Author
Mark Chen – Senior Mechanical Engineer, Peakroc®
Mark Chen is a senior mechanical engineer at Peakroc®, specializing in compressed air systems and drilling equipment for mining and construction applications. With over 15 years of field experience, he has led multiple projects on optimizing air delivery efficiency, equipment durability, and energy consumption.