30–40 Bar Oil-Free High-Pressure Air Compressor Guide for PET Bottle Blowing and Clean Industrial Applications: CFM/FAD, Booster vs Dedicated Compressor, Dryer, Receiver, ISO 8573-1, Pressure Drop, and Air Recovery
30–40 bar is a pressure class, not a complete system specification. A high-pressure application also needs enough FAD at that pressure, stable delivery, the required air purity, correct pressure dew point and adequate storage.
For PET bottle blowing, final forming commonly operates in roughly the 25–40 bar range, but the actual pressure and airflow should come from the blow-molder specification rather than a generic rule. Oil-free high-pressure air is widely used to reduce contamination risk in food and beverage packaging.
Peakroc’s 35 Bar High-Pressure Compressor Guide demonstrates why FAD at pressure matters. The PRMD-3335 delivers approximately 33 m³/min at 35 bar, but it is a drilling-oriented diesel compressor and should not be treated as an oil-free PET product.
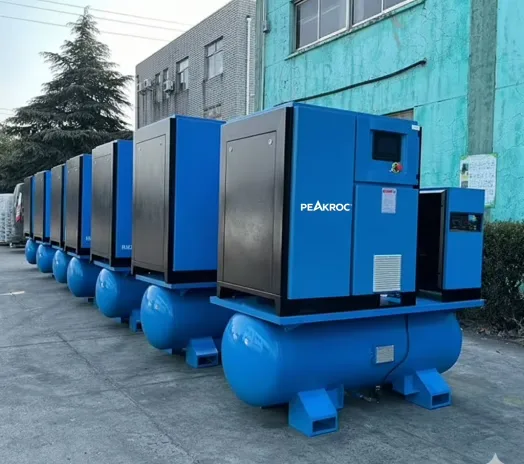
Peakroc’s 16–20 Bar Integrated 4-in-1 Air Compressor combines compressor, receiver, dryer and filtration. It does not provide 30–40 bar PET final-blow pressure, but it demonstrates the integrated architecture required when pressure + storage + moisture control + filtration must work together.
Air quality should be expressed with measurable limits. ISO 8573-1 classifies compressed-air purity by particles, water and oil; the exact class required should come from the process or equipment specification.
Dryer selection should follow the required pressure dew point rather than simply choosing the driest available technology. Peakroc’s Pressure Dew Point Guide explains this relationship in more detail.
A request such as:
“We need a 40 bar oil-free compressor.”
sounds specific.
It is not.
It tells the supplier the approximate pressure class, but it does not tell them how much air the process requires, what purity level is acceptable, how quickly demand changes, how much pressure will be lost through treatment and piping, or whether the system should use a dedicated high-pressure compressor or a booster.
For PET bottle blowing and other clean high-pressure processes, the better engineering sequence is:
Process Demand → Required Pressure → FAD → Air Quality → Dryer → Compressor / Booster → Receiver → Distribution → Point-of-Use Verification
Why 30–40 Bar Oil-Free Air Is a System, Not Just a Compressor
General factory compressed air often operates around 7–10 bar.
Clean high-pressure applications are different.
PET bottle blowing is the best-known example because heated PET preforms must be expanded rapidly against the mold surface using stable high-pressure compressed air.
Industry technical guidance places typical PET final-blowing pressure broadly around 25–40 bar, with process consistency depending not only on pressure but also on flow and purity.
But PET is not the only reason to engineer clean high-pressure air.
Oil-free high-pressure compressor and booster systems are also used in areas such as:
food and beverage processing;
instrument air;
pharmaceutical and cosmetic container production;
industrial gases;
high-pressure clean process air;
selected testing and manufacturing processes.
Commercial oil-free booster systems currently cover roughly 25–42 bar and FAD ranges from approximately 11 to 68 m³/min, demonstrating how widely high-pressure clean-air requirements can vary.
The engineering principle is the same:
Pressure tells you whether the air can perform the work. FAD tells you whether it can continue performing that work.
Size the Compressor by FAD at the Required Pressure
A quotation that only says:
Maximum Pressure: 40 bar
is incomplete.
Suppose two compressors can both reach 40 bar.
One delivers:
6 m³/min @ 40 bar
while another delivers:
20 m³/min @ 40 bar.
They serve completely different production requirements.
For PET, the correct starting point is normally the blow-molding machine specification:
Bottle Format + Production Rate + High-Pressure Air Consumption + Required Inlet Pressure
Bottle volume and BPH help describe the production load, but they should not replace the blow-molder’s actual air-consumption data.
A 1 L bottle does not always consume the same amount of compressed air because preform weight, bottle geometry, stretch ratio, blow sequence and machine design all influence demand.
Example
Suppose a plant operates two blow molders.
Each machine requires:
420 Nm³/h
of high-pressure air.
Both can operate simultaneously.
Gross demand:
420 + 420 = 840 Nm³/h
or:
14 m³/min
If the validated production system recovers 25% of that air:
14 × 0.75 = 10.5 m³/min net demand
If the engineering design then adds a justified 10% operating margin:
10.5 × 1.10 = 11.55 m³/min
The high-pressure system therefore needs approximately:
Peakroc currently publishes the PRMD-3335 at approximately:
33 m³/min 35 bar / 508 PSI 522 kW
The machine is designed for deep drilling, geothermal and other high-pressure field applications.
That makes it relevant to this article for one specific reason:
it demonstrates the relationship between very high airflow and sustained 35 bar pressure.
It should not be presented as a PET food-and-beverage compressor.
Its current positioning is:
diesel + mobile + drilling/high-pressure field duty
rather than:
electric + oil-free + food/beverage process air.
However, the underlying sizing lesson transfers directly:
35 bar without sufficient FAD is useless; high FAD without the required pressure is equally useless.
This is also why Peakroc’s Compressor Finder separates pressure and air capacity instead of treating them as one number.
Peakroc PRMEL: Clean-Air Architecture Reference
Peakroc® PRMEL 16–20 bar integrated compressed-air system combines compressor, air receiver, refrigerated dryer, and precision filtration. For 30–40 bar clean high-pressure applications such as PET bottle blowing, the same treatment principles can be combined with a suitable oil-free high-pressure compressor or booster.
At the other end of the design problem is Peakroc’s PRMEL system.
instead of treating the compressor as an isolated machine.
For an actual 30–40 bar oil-free system, the same architecture can be extended using a suitable oil-free compressor/booster and high-pressure-rated receiver, treatment equipment and piping.
Oil-Free Should Be a Measurable Specification
Terms such as:
clean air
food-grade air
and:
oil-free air
can be too vague for an RFQ.
ISO 8573-1 provides a clearer framework because it defines compressed-air purity according to:
particles + water + oil.
For PET and food/beverage projects, the equipment supplier or plant quality team should specify the required air-quality limits at the actual point of use.
This matters because these are not technically identical:
oil-free compression
and:
oil-lubricated compression followed by downstream oil-removal filtration.
Peakroc’s current PRMEL page describes clean, dry air produced through integrated drying and multi-stage oil/water removal, but PET projects should still define an explicit guaranteed ISO 8573-1 purity requirement instead of assuming that one generic “oil-free” claim satisfies every beverage process.
The relevant measurement point is:
air arriving at the production machine
not only the compressor outlet.
Dryer and Dew Point Matter More as Pressure Increases
Compression concentrates water vapor.
When compressed air cools through aftercoolers, receivers and piping, that moisture can condense.
That makes drying an essential part of many clean high-pressure systems.
The correct question is not:
“Do we need a dryer?”
It is:
“What pressure dew point must be guaranteed under our actual operating conditions?”
For some applications, refrigerated drying may provide adequate moisture control.
Other applications require significantly lower PDP and therefore desiccant drying.
Peakroc’s current Refrigerated vs Desiccant Air Dryer Guide explains why dryer selection should follow the PDP requirement, purge consumption, pressure loss and lifecycle cost.
The dryer must also be sized for:
actual inlet temperature + airflow + pressure + ambient conditions
rather than simply matching compressor motor kW.
Receiver Storage Stabilizes the High-Pressure System
PET blowing creates cyclic demand.
The compressor or booster produces air relatively continuously.
The blow-molding machine consumes it in rapid repeating cycles.
A high-pressure receiver helps separate those two behaviors.
Its main purposes include:
buffering short demand peaks, reducing pressure fluctuation and stabilizing booster operation.
However:
A larger receiver cannot correct permanently insufficient compressor FAD.
If production continuously consumes:
15 m³/min
and the compressor only supplies:
12 m³/min
the receiver eventually loses pressure.
So the sizing order should always be:
Continuous FAD first → Receiver volume second
not the other way around.
Pressure Drop Must Be Budgeted Before Selecting 30, 35 or 40 Bar
The blow molder or production machine does not care what pressure exists inside the compressor.
It cares about the pressure arriving at its inlet.
**Required Compressor/Booster Pressure = Required Process Pressure
Treatment Loss
Distribution Loss
Control Margin**
This also explains why automatically selecting 40 bar “for safety” is poor engineering.
If the process only requires 30 bar and the network can deliver it reliably at 32 bar compressor discharge, continuously producing 40 bar can add unnecessary compression cost.
Peakroc Case: High Pressure and Clean Air Solve Two Different Problems
Peakroc’s existing projects demonstrate two separate pieces of the high-pressure design problem.
In a high-pressure geothermal drilling project, Peakroc used 39 m³/min at 25 bar and deliberately selected large-diameter dual air hoses to reduce pressure loss over the delivery path. The project ultimately reached 1,215 m depth, illustrating how compressor capacity alone is not enough if distribution wastes pressure.
That project was not food-grade and should not be described as such.
But the transferable engineering lesson is directly relevant to 30–40 bar clean-air systems:
Pressure at the compressor is not pressure at the process.
Peakroc’s PRMEL clean-air system demonstrates the other half of the equation:
Air treatment is part of the production system—not an accessory added after compressor sizing.
Together, those experiences support a broader design philosophy:
High pressure must survive distribution, and clean air must survive treatment and delivery.
Air Recovery Can Change the Required Compressor Size
PET blowing is unusual because some of the compressed air discharged after the high-pressure blow cycle can potentially be reused.
Depending on machine design, recovered air may support:
pre-blow air, lower-pressure machine air or another plant-air user.
This can materially reduce net high-pressure compressor demand.
The correct sizing formula becomes:
Gross Blow-Air Demand − Verified Recovered Air = Net High-Pressure Demand
Do not use a brochure’s maximum recovery percentage automatically.
Recovery depends on:
bottle recipe;
bottle size;
blowing pressure;
machine cycle;
recovery valve configuration;
availability of a useful lower-pressure air consumer.
The blow-molder supplier should provide the guaranteed recovery figure for the actual production recipe.
What Should a 30–40 Bar Oil-Free Compressor RFQ Include?
A useful RFQ should give the compressor supplier enough information to design the entire air system.
At minimum, provide:
Application: PET bottle blowing, food/beverage, instrument air or other clean process.
Required pressure at point of use: bar(g) or PSI.
Required FAD: Nm³/h, m³/min or CFM at the stated operating condition.
Demand profile: minimum, normal and peak simultaneous demand.
Required air quality: ISO 8573-1 particle, water and oil class.
Required PDP: at the relevant pressure.
Existing plant-air pressure and capacity: if a booster is being considered.
Receiver and piping information: including distance to process.
Ambient temperature and cooling conditions.
PET data where applicable: bottle formats, BPH, simultaneous blow molders and verified recovery.
With that information, the supplier can determine whether the better architecture is:
Dedicated 40 Bar Oil-Free Compressor
or:
Oil-Free Base Compressor + Dryer + Booster + HP Receiver
rather than guessing from one pressure number.
Final Recommendation
A 30–40 bar oil-free compressed-air system should not be selected by pressure alone.
PET bottle blowing is an important application, but the same engineering principles also apply to other clean high-pressure industrial processes.
Begin with:
required FAD + required point-of-use pressure + required air quality
Then determine the system architecture.
Peakroc’s current product portfolio already demonstrates both sides of the engineering problem:
PRMD-3335 → sustained 35 bar high-pressure capability
They should not be presented as interchangeable products.
Instead, they show why a future 30–40 bar oil-free solution must combine:
high-pressure capability + clean-air architecture
in one engineered system.
The final selection sequence should be:
Application → FAD → Pressure → Air Quality → PDP → Dedicated Compressor or Booster → Receiver → Piping Loss → Recovery → Point-of-Use Verification
The right product is not simply:
“a 40 bar compressor.”
It is:
a complete air system capable of delivering the required amount of clean, dry air at the required pressure where production actually uses it.
FAQ
Is 30 bar enough for PET bottle blowing?
It can be for some bottle and blow-molder designs. Other recipes require 35 or 40 bar. Use the blow-molder manufacturer’s validated pressure specification rather than choosing a universal pressure.
Does PET bottle blowing require an oil-free compressor?
PET food and beverage production commonly uses oil-free high-pressure compressed air to reduce contamination risk. The required oil, water and particle limits should be specified at the point of use using the process specification and ISO 8573-1 framework.
What is the difference between a dedicated high-pressure compressor and a booster?
A dedicated high-pressure compressor produces final pressure directly. A booster receives lower-pressure compressed air and raises it to the required high-pressure level. Booster systems can be attractive when sufficient oil-free base air already exists.
Can Peakroc PRMD-3335 be used directly for PET bottle blowing?
It should not be presented as a direct PET solution. It is currently positioned as a 33 m³/min, 35 bar diesel high-pressure compressor for drilling and demanding field applications, not as a certified oil-free food-and-beverage compressor.
Can Peakroc PRMEL 16–20 bar compressor run a 30–40 bar PET blow molder?
Not directly. Its pressure is below typical 30–40 bar PET final-blow requirements. Its value in this context is as an example of integrated compressor, receiver, dryer and filtration architecture.
Can a booster raise a 16–20 bar system to 30–40 bar?
Potentially, if the upstream compressor provides the inlet pressure, air quality and continuous FAD required by the specific booster. The complete system must be engineered from the booster’s actual inlet and outlet performance data.
Why does a 30–40 bar system need a receiver?
High-pressure processes can have rapid demand fluctuations. A correctly sized receiver stabilizes pressure and buffers short peaks, but it cannot replace insufficient continuous compressor capacity.
5/5 - (1 vote)
Author
Mark Chen – Senior Mechanical Engineer, Peakroc®
Mark Chen is a senior mechanical engineer at Peakroc®, specializing in compressed air systems and drilling equipment for mining and construction applications. With over 15 years of field experience, he has led multiple projects on optimizing air delivery efficiency, equipment durability, and energy consumption.