Key Takeaways
- Airend failure must be confirmed, not assumed. Low pressure or reduced airflow does not automatically mean damaged rotors or bearings. Begin by distinguishing internal mechanical problems from external faults using the portable screw compressor low-airflow troubleshooting guide.
- Bearing noise, vibration and falling FAD are important warning signs. An airend with deteriorating bearings or increased rotor clearances may gradually lose efficiency before complete failure occurs. These symptoms become more meaningful when supported by consistent operating measurements.
- Oil contamination can reveal developing mechanical damage. Water, degraded lubricant and wear particles may indicate elevated risk, but oil contamination is not the same as oil carryover. The oil separator failure and oil carryover guide explains the distinction.
- Rebuilding is economical only when precision components remain serviceable. Replacing bearings and seals may restore an airend with limited damage. Severe rotor scoring, seizure or housing deformation can make replacement more appropriate.
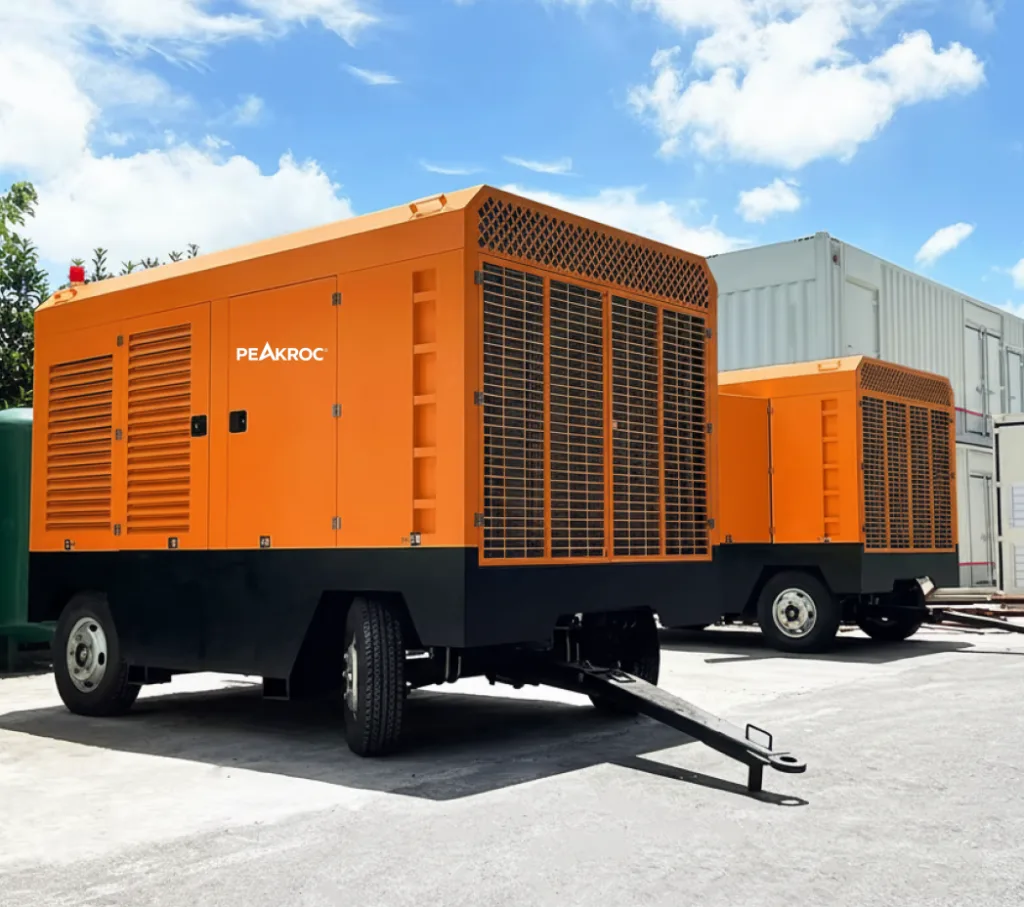
- Complete compressor replacement is a separate purchasing decision. If major airend damage is combined with extensive machine wear or unsuitable capacity, buyers may compare complete units such as the Peakroc® 22 m³/min at 20 bar portable diesel air compressor and 34 m³/min at 25 bar high-pressure compressor, subject to actual operating requirements.
The airend is the core compression assembly of an oil-injected rotary screw compressor. When it deteriorates, the machine may continue operating while producing less usable compressed air, more vibration, abnormal mechanical noise or higher operating temperatures.
For mining contractors, drilling companies, construction equipment operators and industrial maintenance teams, suspected airend failure creates an expensive decision.
Should the technician replace bearings, rebuild the compressor element, purchase a replacement airend or retire the entire machine?
The answer depends on the failure mechanism, the condition of precision components and whether the compressor can deliver its required Free Air Delivery (FAD) after repair.
The central engineering principle is simple: an airend should be condemned only when the available evidence supports internal mechanical damage or unacceptable performance deterioration.
What Is a Rotary Screw Compressor Airend?
An airend, also called a screw element, is the assembly responsible for compressing air inside a rotary screw compressor.
In a typical oil-injected design, two intermeshing helical rotors rotate inside a precisely machined housing. As the rotors turn, air enters the compression chamber, becomes trapped between the rotor profiles and housing, and is compressed as the available volume decreases.
The male and female rotors must operate with carefully controlled clearances. Bearings support their radial and axial positions, while lubricant helps cool, seal and protect the compression assembly.
Why Rotor Clearances Matter
A rotary screw compressor does not depend on mechanical contact between its rotor profiles to create compression.
Instead, its internal geometry and narrow clearances limit the amount of compressed air leaking backward through internal leakage paths.
When the rotor geometry or running position changes, internal leakage may increase.
This can reduce volumetric efficiency, meaning the airend delivers less useful air than expected at a given rotational speed and operating pressure.
Bearing condition is particularly important because worn or damaged bearings may allow excessive shaft movement.
Once movement exceeds the designed tolerance, rotor contact with adjacent surfaces becomes possible.
That can transform a serviceable bearing problem into damage involving rotors, end covers and the housing.
Airend Damage Versus External Compressor Problems
An air compressor is a complete mechanical and control system, not just a screw element.
Reduced air delivery can result from inlet restrictions, loading-control faults, inadequate drive speed or downstream losses even when the airend remains mechanically healthy.
Likewise, high discharge temperature can be caused by poor cooling performance without permanent rotor damage.
Therefore, the first objective is to identify whether the fault originates inside the airend or elsewhere in the compressed-air system.
This distinction prevents unnecessary replacement of one of the machine’s most expensive assemblies.
Rotary Screw Compressor Airend Failure: Diagnostic Symptoms
Airend deterioration can produce different symptoms depending on whether the main problem involves bearings, rotor surfaces, lubrication, temperature or mechanical alignment.
The following table provides a practical diagnostic reference.
| Observable Symptom | Possible Internal Airend Failure | What Must Be Ruled Out | Recommended Confirmation |
|---|---|---|---|
| Gradual FAD or capacity loss | Increased internal leakage, rotor wear, excessive clearance | Intake restriction, inlet valve, reduced RPM | Controlled FAD test at rated operating pressure |
| Whining, rumbling or grinding | Bearing fatigue, poor lubrication, rotor contact | Engine, coupling, fan or motor bearings | Vibration analysis and mechanical inspection |
| Increased vibration | Bearing damage, rotor imbalance, abnormal clearance | Misalignment, loose mounting or drive faults | Trend-based vibration measurements |
| Abnormal airend temperature | Friction, lubrication failure or inefficient compression | Cooler, oil circuit, ambient conditions | Temperature and lubrication-system assessment |
| Metal particles in oil | Bearing, rotor or housing wear | Residual contamination, other lubricated components | Laboratory oil analysis and debris inspection |
| Seizure or inability to rotate | Severe bearing failure or rotor-to-housing contact | Locked drive components or mechanical coupling | Qualified mechanical inspection after isolation |
The table is intended to help narrow the investigation. It is not a substitute for compressor-specific service limits or professional inspection.
Five Warning Patterns That Require Closer Investigation
The following operating patterns deserve particular attention:
- Progressive capacity reduction: The machine delivers less FAD under comparable pressure, speed and inlet conditions despite normal loading controls.
- New mechanical noise: A previously stable compressor develops persistent whining, rumbling or metallic sounds that appear to originate from the airend.
- Increasing vibration: Condition-monitoring measurements show a repeatable rise or a new frequency pattern associated with mechanical deterioration.
- Abnormal oil findings: Laboratory analysis shows concerning changes in wear metals, contamination, viscosity or oxidation relative to previous samples.
- Multiple symptoms occurring together: Declining capacity appears alongside increasing noise, vibration or abnormal temperature.
The final pattern is particularly significant.
A compressor with lower measured FAD and rising bearing-related vibration provides stronger evidence for airend inspection than one with a low-pressure complaint alone.
However, symptom correlation is evidence for further investigation, not proof of a specific failed component.
What Causes Internal Airend Failure?
The principal mechanisms affecting rotary screw compressor airends involve lubrication, contamination, bearing condition, mechanical alignment and operating conditions.
These factors often interact rather than occurring independently.
Main Mechanical and Lubrication Failure Mechanisms
- Lubrication starvation: Insufficient oil delivery reduces the protective lubricant film, increases friction and may damage bearings and other internal surfaces.
- Bearing fatigue and wear: Rolling-contact damage or lubrication-related deterioration can alter rotor positioning and increase the risk of internal contact.
- Abrasive contamination: Dust or solid particles entering the compressor can damage precision surfaces and accelerate wear.
- Oil degradation or moisture contamination: Oxidation, water ingress and unsuitable lubricant characteristics can reduce bearing protection and increase corrosion risk.
- Misalignment or abnormal mechanical loading: Drive-system problems, incorrect assembly or excessive loads can contribute to vibration, bearing stress and premature damage.
How Bearing Failure Becomes Rotor Damage
A bearing supports the rotor shaft in a defined position.
When its rolling elements or raceways deteriorate, rotational stability may decline.
Depending on the bearing design and failure severity, additional radial or axial movement can occur.
This movement may reduce the intended clearance between the rotor and adjacent internal surfaces.
If metal-to-metal contact develops, scoring and additional heat generation can accelerate damage.
The consequences may extend beyond the original bearing.
Repair work can then require inspection of rotor profiles, housing dimensions and end-cover surfaces.
Replacing a damaged bearing without verifying internal geometry may leave the real mechanical problem unresolved.
How Oil Contamination Accelerates Wear
Compressor oil performs several functions in an oil-injected screw element.
It lubricates moving components, removes compression heat and helps seal internal clearances.
When the oil becomes contaminated, its protective performance may deteriorate.
Abrasive particles can contribute to mechanical wear, while water contamination may encourage corrosion or disrupt lubrication.
Oxidation and incorrect viscosity can further compromise operating conditions.
Oil analysis can provide early warning, but interpretation requires care.
Elevated iron content, for example, does not prove that a particular bearing has failed. It may reflect wear involving different ferrous components exposed to the same oil circuit.
Trend data, particle characteristics and mechanical measurements help make the assessment more reliable.
Why Airend Wear Can Reduce Compressor Capacity
Capacity loss is one of the most commercially important consequences of airend deterioration.
In a healthy oil-injected rotary screw compressor, rotor geometry, lubricant sealing and controlled clearances help limit internal air leakage.
When these characteristics deteriorate, more air may circulate through internal leakage paths instead of contributing to useful discharge flow.
The effect can become more noticeable at higher pressure differentials.
Understanding the Difference Between Pressure and FAD
Pressure describes the force available in the compressed-air system.
FAD describes the amount of air delivered, referenced to specified inlet conditions.
A compressor may still achieve its rated pressure when connected to a small load while failing to maintain that pressure at its intended full-flow demand.
This is why an unloaded or low-demand pressure reading cannot confirm airend capacity.
Consider a hypothetical compressor originally rated at 20 m³/min at 13 bar.
During a controlled performance test, it now delivers 17 m³/min at the same specified pressure and rotational speed.
That represents an apparent capacity reduction of approximately 15%.
However, this observation does not establish the root cause.
Before diagnosing worn rotors, the technician must verify comparable inlet conditions, accurate flow measurement, proper inlet-valve opening, adequate drive speed and acceptable external losses.
Only then does reduced internal compression efficiency become a stronger explanation.
Why Capacity Loss Matters on Drilling and Mining Sites
Portable diesel compressors often power equipment that requires continuous airflow under load.
For example, a DTH drilling system needs sufficient air pressure for hammer operation and adequate airflow for cuttings removal.
If a worn compressor element delivers less air than required, drilling productivity may deteriorate even though the compressor continues running.
The equipment may experience unstable tool performance, longer operating periods or reduced hole-cleaning effectiveness.
The economic impact should therefore be evaluated in terms of useful output, fuel consumption and downtime—not merely whether the compressor engine starts successfully.
How to Confirm Airend Failure Before Disassembly
A reliable diagnosis uses repeatable measurements and avoids unnecessary internal work.
The goal is to establish whether there is credible evidence of airend deterioration before authorizing a costly rebuild.
Five-Step Airend Diagnosis Checklist
- Step 1 — Establish the baseline. Record compressor model, operating hours, specified FAD, rated working pressure, loaded RPM, fault history and recent maintenance.
- Step 2 — Exclude external faults. Verify the intake, loading controls, drive speed, air leaks and discharge-system restrictions before blaming the screw element.
- Step 3 — Conduct a controlled capacity test. Measure actual FAD at a defined operating pressure and compare the result with the machine specification or reliable previous records.
- Step 4 — Evaluate mechanical condition. Review vibration, unusual noise, lubrication performance, oil-analysis results and temperature trends under comparable operating conditions.
- Step 5 — Authorize qualified internal inspection. When evidence supports internal damage, have an experienced specialist assess bearings, rotor surfaces, housing condition and critical clearances against manufacturer specifications.
This sequence provides a more defensible diagnosis than replacing parts based on symptoms alone.
What Vibration Monitoring Can Tell You
Vibration analysis can help identify developing mechanical abnormalities.
For example, a damaged bearing may produce characteristic vibration components associated with its geometry and rotational speed.
A technician can compare these measurements with historical baselines and known operating conditions.
However, diagnosing bearing defects requires appropriate sensor placement, measurement methods and interpretation.
Not every increase in vibration originates inside the airend.
Drive misalignment, loose supports and other rotating equipment can create similar signals.
For this reason, vibration analysis works best alongside oil analysis and compressor performance data.
When Should the Compressor Be Shut Down?
Severe grinding, evidence of internal mechanical contact, significant metallic debris or repeated protective shutdowns should be treated as serious warning conditions.
Do not continue operating a machine with suspected seizure or severe mechanical damage simply to complete a shift.
Before inspection, isolate the equipment, prevent unintended restart, allow components to cool where required and verify complete depressurization.
Residual pressure and hot oil can cause severe injuries.
Internal disassembly and rotor-clearance adjustment should be carried out only by qualified personnel using the correct service procedures.
Rotary Screw Compressor Airend Rebuild vs Replacement
Once internal damage has been confirmed, the next decision is whether the existing airend can be restored economically.
An airend rebuild generally involves inspection, replacement of serviceable components and precision reassembly.
The exact procedure varies by airend design.
A properly executed rebuild may include bearing replacement, seal renewal, dimensional measurements, clearance verification and post-repair testing.
An airend replacement involves installing a compatible new or remanufactured compressor element.
Neither option should be selected solely on initial quoted price.
Five Factors for the Rebuild-or-Replace Decision
- Rotor condition: If rotor profiles remain within acceptable limits, rebuilding may be possible. Severe scoring, cracking or dimensional damage can favor replacement.
- Bearing and housing condition: Localized bearing wear may be repairable, while damaged bearing seats or distorted housing surfaces can make rebuilding more difficult.
- Repair quality and parts availability: A rebuild requires suitable replacement components, precision measuring equipment and qualified assembly personnel.
- Downtime and warranty: Consider repair lead time, availability of exchange units, acceptance testing, warranty coverage and the cost of lost production.
- Remaining compressor life: Evaluate the condition of the engine or motor, drive, cooling system, controls and chassis before investing heavily in an older machine.
When Is Rebuilding the Better Option?
Rebuilding can be appropriate when wear has been detected before extensive secondary damage.
For example, an airend with deteriorating bearings but acceptable rotor profiles, housing dimensions and end-cover surfaces may be suitable for a controlled rebuild.
The repair provider should demonstrate that the assembly can be restored to the applicable dimensional and operating requirements.
The report should identify the damaged components, record critical measurements and explain the testing procedure.
A successful rebuild must restore more than mechanical rotation.
It must deliver acceptable operating behavior under the intended conditions.
When Is Replacement More Economical?
Replacement may be preferable when the airend has extensive internal damage.
Severe rotor contact, seized bearings with secondary housing damage, cracked precision components or unacceptable clearances may require repair work that exceeds the value of the existing element.
Replacement can also reduce downtime when a compatible exchange unit is available and a specialized rebuild would require extensive machining or parts procurement.
Compatibility must be confirmed using exact model information.
Similar-looking airends are not necessarily interchangeable.
Rated speed, compression capacity, pressure range, drive connection, mounting arrangement and lubrication requirements can all differ.
Total Cost of Repair Versus Replacement
A useful decision should consider the complete recovery cost:
Total Recovery Cost = Airend Repair or Replacement + Labor + Associated Component Work + Oil-System Decontamination + Logistics + Downtime
This is a cost-accounting framework, not a fixed pricing formula.
The actual calculation should also consider warranty, remaining service life and the risk of repeat failure.
A cheaper rebuild can become expensive if underlying damage is missed.
Conversely, replacing a serviceable airend can waste capital that could have been preserved through an appropriate repair.
The goal is to restore dependable compressed-air production at a justifiable lifecycle cost.
How to Evaluate a Completed Airend Rebuild
A repaired airend should not be accepted solely because it rotates freely or the compressor can restart.
Mechanical restoration and performance restoration are related but different.
Dimensional Inspection and Assembly Quality
The repair documentation should confirm that critical dimensions were checked against the applicable airend specifications.
Depending on the design, inspection may involve bearing locations, rotor condition, housing dimensions and axial or radial clearances.
Measurements must be performed with suitable equipment.
Generic clearance values from unrelated compressor models should not be used as acceptance criteria.
Post-Rebuild Performance Verification
Once the airend has been installed and the compressor is ready for a controlled test, performance should be evaluated under appropriate operating conditions.
A useful acceptance test considers the machine’s ability to deliver the required FAD at the specified pressure and speed.
Mechanical noise, vibration, temperature, lubrication behavior and leakage should also remain acceptable.
For portable diesel compressors, the drive system and engine operating condition must be taken into account when evaluating compressor performance.
Successful startup does not prove that the airend has recovered its original capacity or mechanical reliability.
Root-Cause Correction
An important part of rebuilding is identifying why the previous airend deteriorated.
If lubrication starvation caused bearing damage, replacing the bearings without correcting the oil-delivery problem leaves the new components exposed to the same risk.
If metallic debris entered the oil circuit, contaminated connected components may require cleaning or replacement according to the applicable repair procedure.
A professional repair should address both the damaged component and the mechanism that caused the damage.
Technical Field References
The following examples are based on publicly documented industry service activities and technical maintenance programs.
They illustrate airend overhaul practices and failure-prevention principles. They are not presented as Peakroc® customer projects or independently measured performance comparisons.
Field Reference 1: Water-Well Compressor Element Overhaul in Maharashtra, India
A manufacturer-published service record documents a screw-element overhaul involving a water-well drilling compressor in Maharashtra, India.
The project appeared within a publicly reported 2020 element-overhaul program.
The published material demonstrates that operators of high-duty drilling compressors may choose a major element overhaul rather than automatically replacing the entire machine.
This distinction is important for equipment owners because the economic decision involves the airend’s condition as well as the remaining value of the compressor.
Engineering lesson: A screw-element overhaul can be a distinct maintenance option between routine servicing and complete compressor replacement.
The public record does not establish the original failure mechanism, measured bearing damage or exact FAD improvement. Those results should not be inferred.
Field Reference 2: Water-Well Compressor Refurbishment in Ranchi, India
Another manufacturer-published project documents refurbishment of a portable water-well drilling compressor operated by a customer in Ranchi, India.
The same refurbishment program distinguishes service packages that include element overhauling from packages that include complete airend replacement.
This illustrates why equipment refurbishment should not be treated as one standardized operation.
Different machines may require different levels of mechanical intervention.
Engineering lesson: The scope of refurbishment should depend on inspected component condition, not simply the compressor’s age.
The published project confirms that refurbishment occurred, but it does not provide independently verified airend-failure measurements or a quantified recovery in air delivery.
Field Reference 3: Specialist Airend Rebuilding Workshop Procedures
A specialist compressor rebuilding workshop publicly describes an airend rebuilding process involving disassembly, component inspection, dimensional recording, cleaning, repair and reassembly.
The workshop process emphasizes checking individual parts and documenting wear before deciding which components can be reused.
This is relevant because airend refurbishment is precision mechanical work, not merely a bearing replacement procedure.
Engineering lesson: Successful rebuilding depends on identifying damaged surfaces, measuring critical components and restoring the assembly to acceptable operating tolerances.
The published workshop description provides evidence of an established rebuilding workflow. It is not an independently verified customer case showing specific fuel savings, compressor capacity gains or longer bearing life.
How to Prevent Premature Airend Failure
Preventive maintenance should protect the mechanical conditions on which the screw element depends.
Maintaining the correct lubricant level and specification helps preserve lubrication, cooling and sealing.
Effective air filtration limits the entry of abrasive particles.
Appropriate cooling-system maintenance reduces the risk of excessive temperature and lubricant degradation.
For compressors in demanding service, oil analysis and vibration monitoring can add information beyond routine visual inspections.
The greatest value comes from trend analysis.
A change in wear-metal concentration or vibration pattern is easier to interpret when historical measurements are available.
Maintenance teams should also review unexpected changes following repairs or equipment relocation.
A compressor that becomes noisier after drive work may require alignment inspection. A machine that begins losing capacity after moving to a higher-altitude site may require performance assessment under the new conditions rather than immediate airend replacement.
Preventive maintenance intervals should follow the specific compressor manufacturer’s instructions.
There is no universal airend replacement hour applicable to every screw compressor.
Actual service life depends on bearing design, lubricant condition, operating load, contamination, temperature, installation and maintenance quality.
Final Recommendation
Rotary screw compressor airend failure is best understood as a mechanical condition that must be established through evidence.
Declining FAD, bearing noise, excessive vibration, overheating and contaminated oil may indicate internal deterioration.
However, these symptoms overlap with faults affecting other compressor systems.
A reliable diagnosis first excludes external causes, then evaluates actual compressor performance and mechanical condition.
When internal damage is confirmed, rebuilding may be economical if the precision components remain serviceable.
Replacement becomes more attractive when severe damage prevents reliable or cost-effective restoration.
For equipment owners, the final decision should consider repair quality, post-rebuild performance, downtime, warranty and the remaining life of the entire compressor.
The best repair is not simply the one that makes the compressor run again. It is the one that restores verified air delivery and mechanical reliability while controlling long-term operating cost.
FAQ
What are the first signs of rotary screw compressor airend failure?
Possible early signs include gradually declining FAD, unusual bearing noise, increasing vibration, abnormal airend temperature and elevated wear-metal levels in compressor oil. These symptoms require further diagnosis because other compressor components can produce similar problems.
Can a worn airend cause low compressor capacity?
Yes. Rotor or housing damage and excessive internal clearances may increase air leakage inside the compression chamber, reducing useful FAD. External restrictions, loading-system faults and operating conditions should be excluded before diagnosing airend wear.
Does bearing noise mean the compressor airend is failing?
Not necessarily. Unusual whining, rumbling or grinding can indicate bearing damage, but similar sounds may come from the engine, motor, coupling or drive system. Vibration measurements and specialist inspection are needed to identify the source.
Can overheating permanently damage a screw compressor airend?
Yes. Severe or repeated overheating can degrade lubricant, increase friction and damage bearings or other internal components. However, overheating alone does not prove permanent airend damage; the cooling and lubrication systems must also be checked.
What do metal particles in compressor oil indicate?
Metal particles may indicate abnormal wear involving bearings, rotors, gears or other oil-contacting components. Oil analysis, particle examination and operating trends help identify the likely source. Significant metallic debris requires prompt investigation.
Is it possible to rebuild a failed rotary screw airend?
Yes, when its rotors, housing and other precision surfaces remain serviceable within the manufacturer’s tolerances. A qualified rebuild may include bearing and seal replacement, dimensional inspection, clearance verification and appropriate testing.
When is replacing an airend better than rebuilding it?
Replacement may be preferable when severe rotor scoring, seizure, housing damage or excessive wear makes rebuilding unreliable or uneconomical. Parts availability, downtime, warranty and the condition of the complete compressor should also be considered.
How long does a rotary screw compressor airend last?
There is no universal service life. Actual longevity depends on design, bearing condition, lubrication, operating load, temperature, contamination and maintenance. Follow the manufacturer’s overhaul recommendations and use condition monitoring rather than assuming failure at a fixed number of hours.
Author
Mark Chen – Senior Mechanical Engineer, Peakroc®
Mark Chen is a senior mechanical engineer at Peakroc®, specializing in compressed air systems and drilling equipment for mining and construction applications. With over 15 years of field experience, he has led multiple projects on optimizing air delivery efficiency, equipment durability, and energy consumption.